Pinch analysis for chemical plants maps every hot and cold process stream to find the lowest energy use a site can reach. It shows how much heat you can recover. It also shows how much steam and cooling water you still need to buy.
Here's the catch. A heat recovery design only saves energy while exchangers stay clean, traps work, and controls hold their setpoints. When fouling builds up, the plant slides back toward its old energy bill without anyone noticing. This guide shows how to tie pinch analysis targets to daily maintenance so the savings last.
Key Takeaways
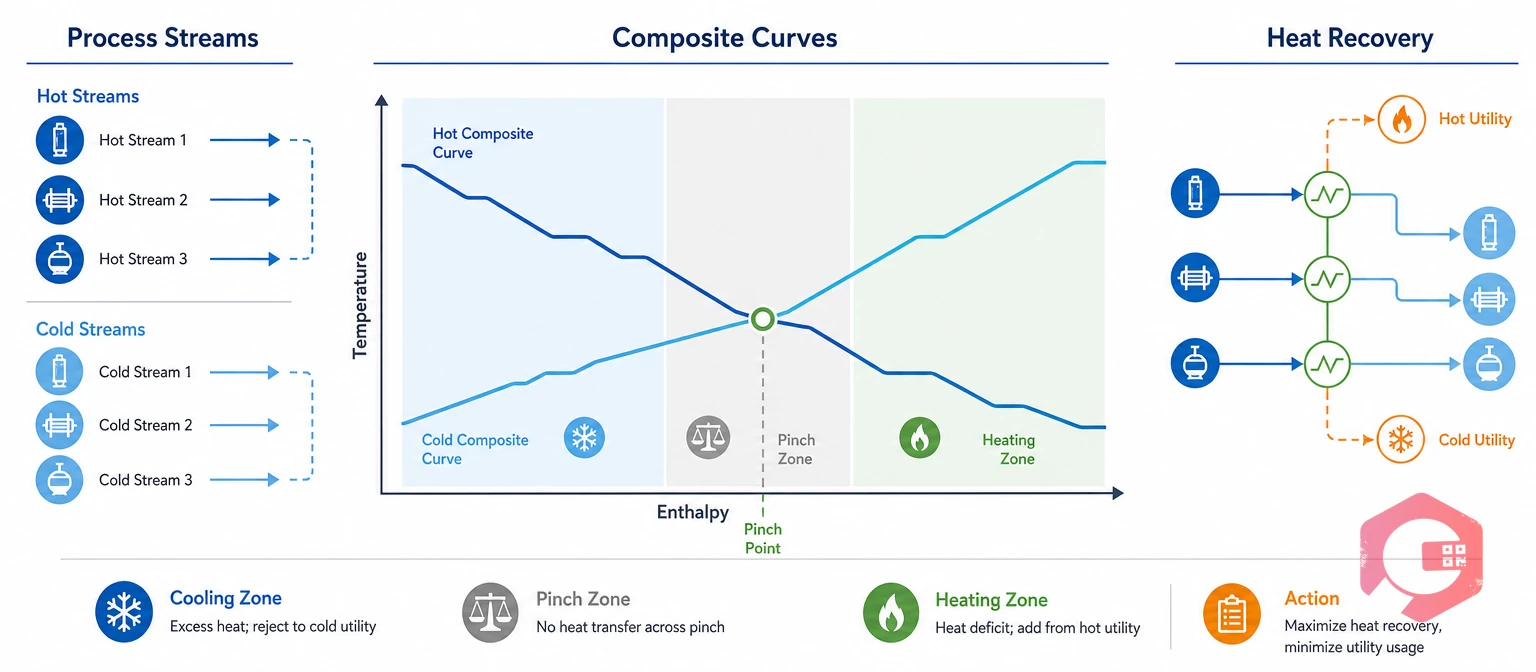
Pinch analysis is an energy targeting method that plots all process heat sources and heat sinks as two composite curves. The point where the curves come closest is called the pinch. You can read more about the method's background on pinch analysis.
The minimum approach temperature (ΔTmin) is the smallest temperature gap you allow between hot and cold streams in an exchanger. A smaller ΔTmin recovers more heat but needs more exchanger area. Most designs follow three simple rules:
These rules sound like design topics, yet maintenance decides whether the plant follows them in daily operation. A fouled exchanger or a leaking bypass valve can break all three rules at once. That is why many chemical sites run energy programs under ISO 50001 energy management. The standard asks for a measured baseline and proof of improvement.
Pinch studies assume clean equipment and steady operation. The table shows where that assumption breaks down and how maintenance closes the gap.
| Area | Design assumption | What happens in the plant | Maintenance response |
|---|---|---|---|
| Heat exchanger network | Clean surfaces at design U-value | Fouling and scaling cut heat transfer, so more steam is needed | Trend approach temperature and clean by condition |
| Steam system | All traps and valves work as intended | Failed-open traps and leaks waste live steam | Run trap surveys and repair leaks on a set cycle |
| Cooling water | Design flow and inlet temperature | Scaling, biofouling, and poor tower performance raise temperatures | Water treatment checks and tower inspections |
| Fired heaters | Tuned burners and low excess air | Burner drift and air leaks raise fuel use | Combustion tuning and stack temperature checks |
| Insulation | Intact lagging on hot lines | Wet or missing insulation loses heat and hides corrosion | Thermography surveys and insulation repair |
| Instruments and controls | Accurate readings and setpoints | Sensor drift moves the plant away from its energy target | Calibration and control loop checks |
Fouling is the gradual build-up of deposits on heat transfer surfaces that cuts an exchanger's performance. Because it grows a little each day, no single shift sees an event worth reporting. Rank each area by energy cost and process risk, not by asset age. A small exchanger near the pinch can matter more than a large utility cooler.
Want to put a number on what these losses cost each year? Try the mean maintenance cost calculator to set a cost baseline before you change anything.

The strongest energy programs treat pinch analysis targets as maintenance targets. This five-step framework turns a one-time study into a routine your crews can follow.
The Pinch-Protect Maintenance Framework:
Link condition monitoring software to plant sensors. Then a rising approach temperature can open a work order before the energy bill shows the loss.
A fixed cleaning calendar wastes effort on clean units and misses fast-fouling ones. A pinch-based schedule sets priority by energy value and lets condition decide the timing.
| Exchanger position | Energy impact | What to monitor | Cleaning trigger |
|---|---|---|---|
| Near the pinch | Highest; small losses raise both heating and cooling | Approach temperature, U-value, pressure drop | Condition limit reached or set run time, whichever comes first |
| Above the pinch | Lost duty is made up with steam or fuel | Hot outlet temperature, steam flow | Rising steam demand at steady throughput |
| Below the pinch | Lost duty is made up with cooling water | Cold outlet temperature, cooling water load | Rising cooling demand or temperature limits |
| Feed-effluent exchangers | Large share of recovered heat | Furnace inlet temperature, fuel use | Fuel use per tonne above baseline |
| Utility heaters and coolers | Direct utility cost | Utility flow and outlet temperature | Performance drop or scheduled shutdown |
Plan large cleanings for turnarounds. Keep bypass and isolation valves in working order, so you can clean one unit while the rest keep running. This approach fits well with condition-based maintenance, where data decides when work is due.
Use this pinch analysis checklist to keep heat recovery performance close to target between studies.
A steam trap is a valve that drains condensate from steam lines while holding live steam in. A trap that fails open blows live steam into the condensate system. A regular survey is one of the cheapest energy checks a site can run.
Most pinch analysis savings are lost through small habits, not big failures. Maintenance teams that keep their energy gains usually avoid these five mistakes.
Fixing these habits costs little and keeps the original study paying back for years.
Exchanger cleaning and line breaks carry real process hazards. Many chemical sites fall under OSHA's Process Safety Management standard, which covers mechanical integrity and management of change.
Linking each cleaning job to its isolation steps and permit keeps energy work as safe as any other mechanical job.

A 90-day start keeps the scope small. It also gives the team a clear result to show operations.
Early results build trust with operations and help justify sensors for the rest of the network.
A Computerized Maintenance Management System gives every exchanger, trap, and heater one record and one history. Energy performance then becomes part of daily maintenance work.
Maintenance teams using Cryotos have reported up to 30% reduction in unplanned downtime and 25% faster repair turnaround. Cryotos does not run pinch calculations itself; it keeps the targets from your study visible in daily work. Most chemical sites start with near-pinch exchangers, then add steam and cooling water systems.
Savings depend on how well the existing network already recovers heat. Many studies find worthwhile savings in older plants, but the gain only lasts if exchangers and utilities are maintained.
Clean them by condition rather than by date. Set limits on approach temperature, U-value, or pressure drop, and plan large jobs for turnarounds.
Fouling, failed steam traps, open bypass valves, and drifting controls slowly undo the design. Regular trending catches these losses early.
Start with exchangers near the pinch and large feed-effluent units. Losses there raise both heating and cooling demand.
Software stores design targets on each asset, collects readings, and opens work orders when limits are crossed. It also links each job to energy and cost results.
Energy savings last when maintenance protects them every day. Schedule a free demo to see how Cryotos turns your pinch targets into tracked, condition-based maintenance work.


Cryotos AI predicts failures, automates work orders, and simplifies maintenance—before problems slow you down.